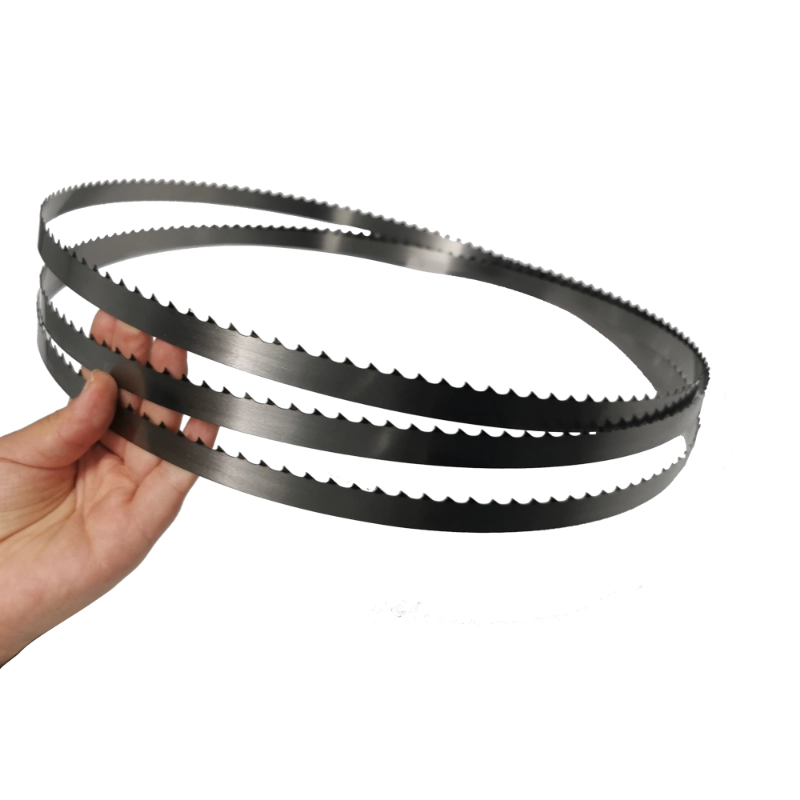
What This Category Solves
Standard-length band saw blades do not fit every saw. Horizontal and vertical band saw machines from different brands and models vary in wheel diameter, center distance, and maximum cutting width. Blade length must match the machine nameplate or technical documentation precisely. Al mismo tiempo, the same machine may cut solid bar, thin-wall tube, acero carbono, or stainless steel—each requiring a different tooth pitch and tooth form. The cost of choosing the wrong blade is not limited to the blade itself; it also includes downtime for blade changes, scrapped workpieces, and delayed delivery.
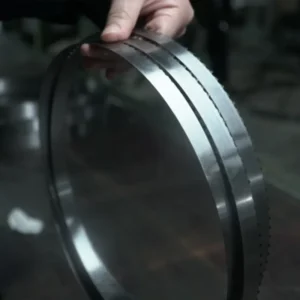
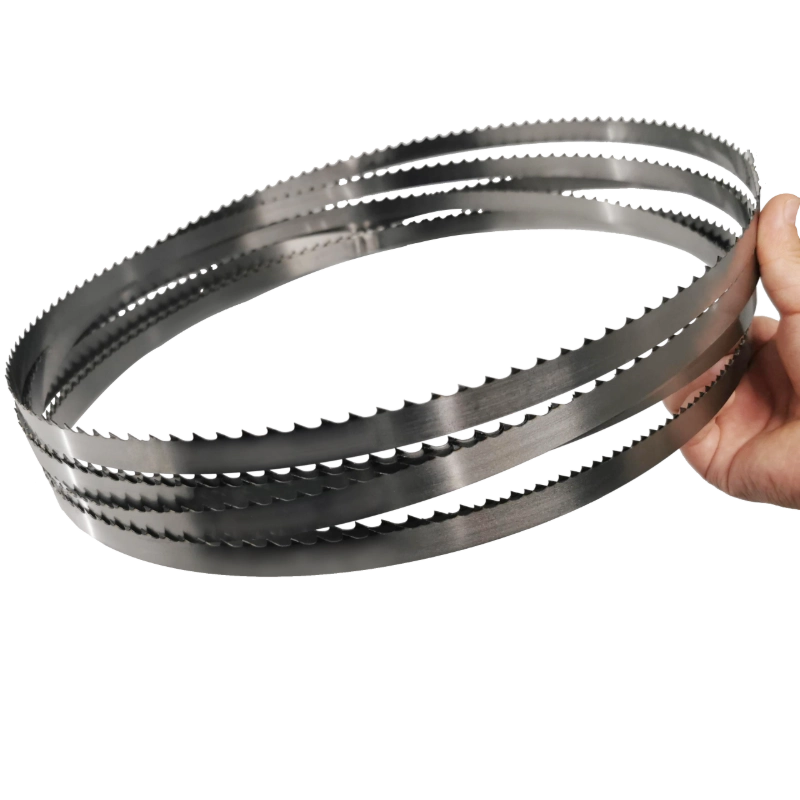
The core value of custom welded band saw blades is “the dimensions fit, the tooth pitch matches, and the joint holds.” The factory welds the blade into a loop based on the machine model or measured length you provide, matches tooth pitch to the workpiece cross-section and material, and delivers it ready to install and run.
Core Specifications and Matching Dimensions
A custom welded band saw blade is defined by four interrelated dimensions. All four must be confirmed.
| Dimensión | Matching Basis | Typical Considerations |
|---|---|---|
| Longitud | Saw brand/model, or measured circumference of the old blade | Wheel diameter, center distance, tension stroke; the welded joint must be accounted for in length compensation |
| Ancho | Maximum/minimum blade width allowed by the machine; workpiece straightness requirements | Greater width improves cutting stability; vertical saws must also consider minimum bend radius |
| Espesor | Machine wheel flange and guide system; workpiece precision requirements | Thickness affects cutting torsional rigidity and cut surface flatness; a machine may accept different thicknesses at the same width |
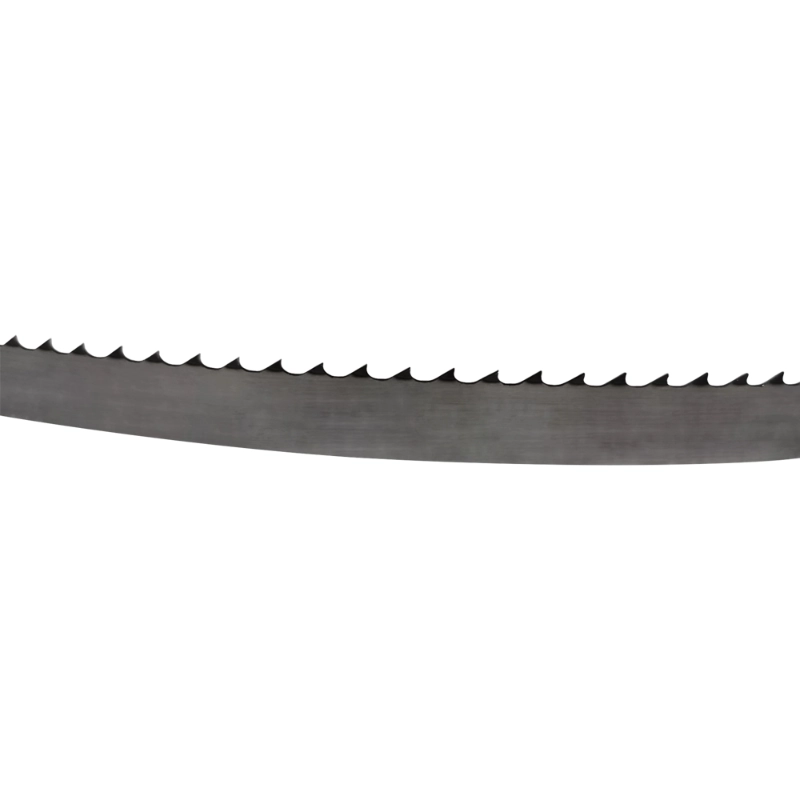
| Tooth pitch | Workpiece material, cross-section size, and shape | Core principle: maintain a reasonable number of teeth in cut at the same time to avoid tooth gullet overload or chip clogging |
Tooth Pitch (TPI) Selection Guide
Tooth pitch selection is the most underestimated step in custom welding. If TPI is too low on thin-wall or small cross-sections, the tooth gullet load becomes excessive and teeth may strip. If TPI is too high on large solid sections, chip evacuation becomes poor and cutting efficiency drops sharply. The following is the industry-common logic linking tooth pitch, cross-section, and material. It is intended for preliminary judgment before inquiry.
Recommended TPI by Workpiece Type
| Workpiece Type | Recommended TPI Range | Selection Logic |
|---|---|---|
| Structural steel / solid bar (large cross-section) | 3–4, 4–6 | Lower TPI provides greater gullet capacity for chip evacuation in large sections |
| Structural steel / solid bar (small cross-section) | 5–8, 6–10 | More teeth in cut distributes cutting force |
| Steel tube / thin-wall profiles | 8–12, 10–14 | Fine pitch helps prevent tooth tip stripping on thin walls and controls burr |
| Aluminum / metales no ferrosos | 3, 4–6, 5–8 | Coarse pitch evacuates chips efficiently and reduces heat buildup in soft metals |
| Acero inoxidable / aleación de acero (M42 bimetal applications) | Select from approximately 10/14 a 5/8 depending on cross-section | Variable pitch helps suppress chatter and vibration marks |
Solid Diameter / Profile Wall Thickness vs. Variable Pitch TPI
| Solid Diameter (milímetros) | Profile Wall Thickness (milímetros) | Recommended Variable Pitch TPI |
|---|---|---|
| 0–20 | 3–5 | 10–14 |
| 10–30 | 4–6 | 8–12 |
| 20–50 | 5–8 | 6–10 |
| 30–60 | 8–10 | 5–8 |
| 50–90 | 12–16 | 4–6 |
| 80–150 | 16–22 | 3–4 |
“Teeth in cut” rule of thumb: A reasonable target range is approximately 3–18 teeth in contact with the widest part of the workpiece. Por ejemplo, a 4/6 variable-pitch blade generally performs well across 25–125 mm section widths (at a 5 TPI average, acerca de 5 teeth in cut on a 1″ section and about 25 teeth in cut on a 5″ section). Provide the workpiece cross-section size and shape in your inquiry, and the factory can confirm whether the tooth pitch matches.
Welded Joint Quality Benchmarks
The life of a custom welded blade often depends less on the tooth tip than on the joint. Industry-common acceptance benchmarks for bimetal band saw blade welds include:
| Indicator | Reference Benchmark |
|---|---|
| Weld tensile strength | ≥ 1200 MPa |
| Weld shear strength | ≥ 800 MPa |
| Fatigue life (pulsating load) | ≥ 10⁶ cycles |
| Tooth pitch tolerance | 0.02 milímetros / 10 teeth |
| Tooth height deviation | ≤ 0.05 milímetros |
Fuente: bimetal band saw blade inspection industry standards. After welding, the joint should be annealed to eliminate brittleness and reduce the risk of fatigue fracture. Specific acceptance criteria and inspection methods are subject to the factory’s quality documentation.
Information Required for Inquiry
This custom welding page does not offer an “add to cart and order immediately” path. Every blade specification must be confirmed by the factory for manufacturability before quotation. To help the factory give an accurate answer on the first response, please provide the following five core pieces of information:
-
Saw machine brand / model — Used to confirm the machine’s allowable blade length, ancho, and thickness range, as well as wheel diameter and guide system constraints.
-
Blade dimensions — Length (preferably the value stated in the machine manual or the measured circumference of the old blade), ancho, and thickness. If uncertain, provide the machine model and the factory can look it up.
-
Workpiece material — Carbon steel, aleación de acero, acero inoxidable, aluminum, metales no ferrosos, etc.. For alloy steel or stainless steel, note the grade or hardness range.
-
Workpiece cross-section — Solid / tube / profile, and the maximum cross-section size (diameter, ancho, wall thickness). This is the decisive input for tooth pitch selection.
-
Cutting objective — Are you prioritizing cutting speed, cut surface quality, blade life, or a balance of all three? Does the application involve bundle cutting or unattended continuous production?
Who It Is For and Typical Scenarios
Maintenance service providers: Customer sites use a wide range of saw brands and models, and stocking standard-length blades cannot cover every machine. Custom welding by model reduces “waiting for the blade while the machine is down” and replaces extensive inventory with specification matching.
Saw machine distributors: The blade length supplied with each machine must correspond exactly to the equipment. Custom welding can be offered as a delivery accessory, reducing after-sales issues caused by blade mismatch at the end customer.
Multi-machine processing plants: One workshop may run horizontal and vertical band saws and cut multiple materials and cross-sections. Custom welding grouped by machine and tooth pitch by application reduces efficiency losses and early failures caused by “making one blade fit everything.”
FAQ
Q: What is the typical lead time for custom welded blades?
A: In industry practice, suppliers with coil stock and welding capability can deliver common specifications within a few business days, and some welding centers dispatch orders received before cut-off on the same day. The actual lead time depends on whether the selected width/thickness/tooth pitch has corresponding coil stock, the welding schedule, and order quantity. It is subject to factory confirmation.
Q: I only know the saw model, not the exact length. Can I place an order?
A: You can submit an inquiry, but the factory must confirm. For most industrial band saws, the length can be obtained from the machine manual or nameplate. If only the model is available, the factory may be able to look up the specification for that model. If the machine has been modified or is non-standard, measuring the old blade circumference or confirming the center distance under tension is still recommended.
Q: What happens if the tooth pitch is wrong?
A: If TPI is too high on a large cross-section, gullet capacity is insufficient, chip evacuation is obstructed, cutting force rises, and tooth tips overheat. If TPI is too low on a thin wall, the load per tooth becomes excessive, causing tooth stripping or thin-wall deformation. The value of a custom page is precisely confirming the tooth pitch and application match before welding, rather than handling returns afterward.
Q: What is the minimum order quantity?
A: MOQs vary widely among factories. Industry practice ranges from single test blades to batch-order minimums. This category is inquiry-based and does not set a uniform committed MOQ. Both small test batches and large production orders must be evaluated by the factory according to the specific specifications.
Q: Does the welded joint affect blade life?
A: Sí. The mechanical properties of the heat-affected zone differ from the base material, and the joint is a sensitive location for fatigue fracture. Recocido, welding parameter control, and joint inspection are key to controlling this risk. During inquiry, you may ask the factory to explain its welding process and joint acceptance benchmarks.